M20D-FKS ENGINE MECHANICAL CYLINDER HEAD REPLACEMENT
PROCEDURE

 11122
1.REPLACE INTAKE VALVE GUIDE BUSH
Heat the cylinder head sub-assembly to between 80 and 100°C (176 to 212°F).
Place the cylinder head sub-assembly on wooden blocks.
- CAUTION:
-
Be sure to wear protective gloves.
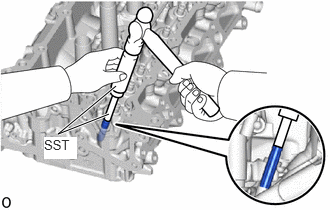
Using SST and a hammer, tap out the intake valve guide bush.
- SST
- 09201-01055
09950-70010 (09951-07100)
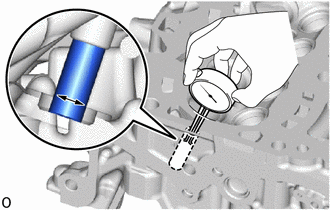
Using a caliper gauge, measure the intake valve guide bush bore diameter of the cylinder head sub-assembly.
- Standard Intake Valve Guide Bush Bore Diameter:
10.285 to 10.306 mm (0.405 to 0.406 in.)
- New Guide Bush Selection Chart:
Bush Size Specified Condition STD 10.333 to 10.344 mm (0.40681 to 0.40724 in.) O/S 0.05 10.383 to 10.394 mm (0.40877 to 0.40921 in.)
- Standard Bush Length:
41.3 to 41.7 mm (1.63 to 1.64 in.)
- HINT:
- ·
If the intake valve guide bush bore diameter of the cylinder head sub-assembly is more than 10.306 mm (0.406 in.), machine the intake valve guide bush bore of the cylinder head sub-assembly to a dimension of 10.335 to 10.356 mm (0.407 to 0.408 in.) to install an O/S 0.05 intake valve guide bush.
·If the intake valve guide bush bore diameter of the cylinder head sub-assembly is more than 10.356 mm (0.408 in.), replace the cylinder head sub-assembly.
Heat the cylinder head sub-assembly to between 80 and 100°C (176 to 212°F).
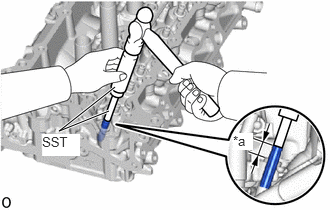
| *a | Protrusion Height |
Using SST and a hammer, tap in the selected intake valve guide bush.
- SST
- 09201-10000 (09201-01050)
09950-70010 (09951-07100)
- Standard Protrusion Height:
13.35 to 13.60 mm (0.526 to 0.535 in.)
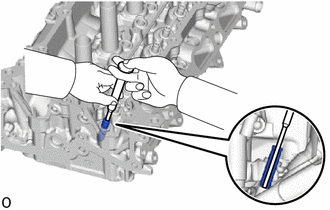
Using a sharp 5.5 mm reamer, ream the intake valve guide bush to obtain the standard oil clearance.
- Standard Oil Clearance:
0.025 to 0.060 mm (0.000984 to 0.00236 in.)
11126
2.REPLACE EXHAUST VALVE GUIDE BUSH
Heat the cylinder head sub-assembly to between 80 and 100°C (176 to 212°F).
Place the cylinder head sub-assembly on wooden blocks.
- CAUTION:
-
Be sure to wear protective gloves.
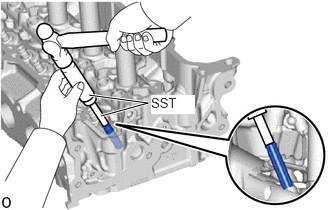
Using SST and a hammer, tap out the exhaust valve guide bush.
- SST
- 09201-01055
09950-70010 (09951-07100)
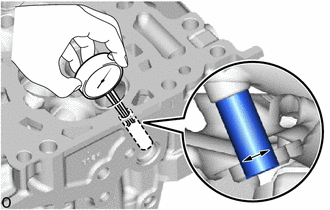
Using a caliper gauge, measure the exhaust valve guide bush bore diameter of the cylinder head sub-assembly.
- Standard Exhaust Valve Guide Bush Bore Diameter:
10.285 to 10.306 mm (0.405 to 0.406 in.)
- New Guide Bush Selection Chart:
Bush Size Specified Condition STD 10.333 to 10.344 mm (0.40681 to 0.40724 in.) O/S 0.05 10.383 to 10.394 mm (0.40877 to 0.40921 in.)
- Standard Bush Length:
43.3 to 43.7 mm (1.70 to 1.72 in.)
- HINT:
- ·
If the exhaust valve guide bush bore diameter of the cylinder head sub-assembly is more than 10.306 mm (0.406 in.), machine the exhaust valve guide bush bore of the cylinder head sub-assembly to a dimension of 10.335 to 10.356 mm (0.407 to 0.408 in.) to install an O/S 0.05 exhaust valve guide bush.
·If the exhaust valve guide bush bore diameter of the cylinder head sub-assembly is more than 10.356 mm (0.408 in.), replace the cylinder head sub-assembly.
Heat the cylinder head sub-assembly to between 80 and 100°C (176 to 212°F).
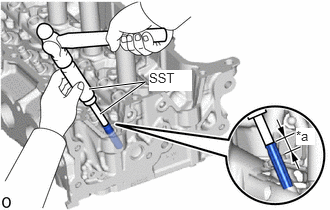
| *a | Protrusion Height |
Using SST and a hammer, tap in the selected exhaust valve guide bush.
- SST
- 09201-10000 (09201-01050)
09950-70010 (09951-07100)
- Standard Protrusion Height:
13.75 to 14.00 mm (0.541 to 0.551 in.)
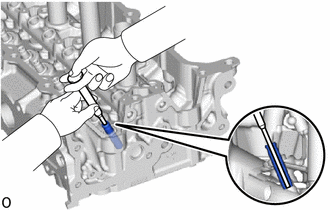
Using a sharp 5.5 mm reamer, ream the exhaust valve guide bush to obtain the standard oil clearance.
- Standard Oil Clearance:
0.030 to 0.065 mm (0.00118 to 0.00256 in.)
11115A
3.REPLACE RING PIN
- NOTICE:
-
It is not necessary to remove the ring pins unless they are being replaced.
Remove the 2 ring pins.
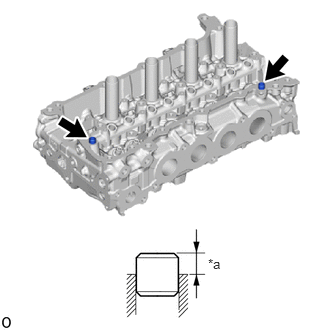
| *a | Protrusion Height |
Using a plastic-faced hammer, tap in 2 new ring pins to the cylinder head sub-assembly.
- Standard Protrusion Height:
6.5 to 7.5 mm (0.256 to 0.295 in.)