M20F-FXS, M20G-FXS ENGINE MECHANICAL CYLINDER HEAD INSPECTION
PROCEDURE

 11101
1.INSPECT CYLINDER HEAD SUB-ASSEMBLY
Using a precision straightedge and feeler gauge, measure the warpage of the contact surfaces where the cylinder head sub-assembly contacts the cylinder block sub-assembly, intake manifold and exhaust manifold.
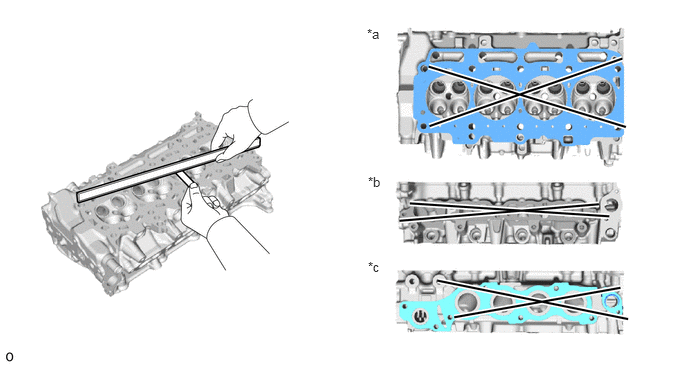
| *a | Bottom Side | *b | Intake Manifold Side |
| *c | Exhaust Manifold Side | - | - |
- Maximum Warpage:
Item Specified Condition Bottom side 0.05 mm (0.00197 in.) Intake manifold side 0.10 mm (0.00394 in.) Exhaust manifold side 0.10 mm (0.00394 in.)
- HINT:
-
If the warpage is more than the maximum, replace the cylinder head sub-assembly.
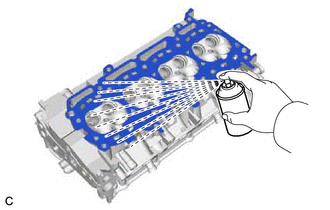
Using a dye penetrant, check the intake ports, exhaust ports and cylinder head sub-assembly surface for cracks.
- HINT:
-
If cracks are found, replace the cylinder head sub-assembly.
2.INSPECT COMPRESSION SPRING
Intake Side:
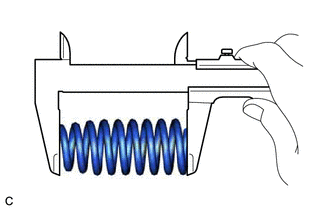
Using a vernier caliper, measure the free length of the compression spring.
- Standard Free Length:
58.81 mm (2.32 in.)
- HINT:
-
If the free length is not as specified, replace the compression spring.
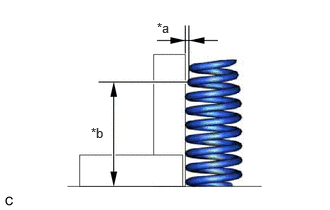
| *a | Deviation |
| *b | 37 mm (1.46 in.) |
Using a steel square, measure the deviation of the compression spring.
- Maximum Deviation (Reference):
1.0 mm (0.0394 in.)
- HINT:
-
If the deviation is more than the maximum, replace the compression spring.
Exhaust Side:
Using a vernier caliper, measure the free length of the compression spring.
- Standard Free Length:
58.81 mm (2.32 in.)
- HINT:
-
If the free length is not as specified, replace the compression spring.
| *a | Deviation |
| *b | 37 mm (1.46 in.) |
Using a steel square, measure the deviation of the compression spring.
- Maximum Deviation (Reference):
1.0 mm (0.0394 in.)
- HINT:
-
If the deviation is more than the maximum, replace the compression spring.
13711
3.INSPECT INTAKE VALVE
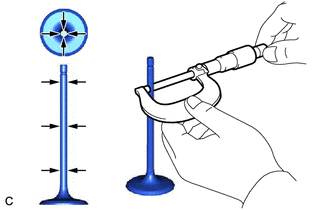
Using a micrometer, measure the diameter of the valve stem.
- Standard Valve Stem Diameter:
5.470 to 5.485 mm (0.215 to 0.216 in.)
- HINT:
-
If the valve stem diameter is not as specified, check the intake valve guide bush oil clearance.
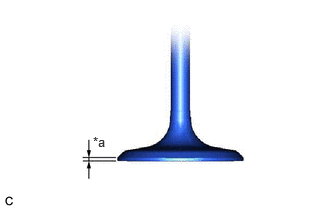
| *a | Margin Thickness |
Using a vernier caliper, measure the valve head margin thickness.
- Standard Margin Thickness:
1.0 mm (0.0394 in.)
- Minimum Margin Thickness:
0.5 mm (0.0197 in.)
- HINT:
-
If the margin thickness is less than the minimum, replace the intake valve.
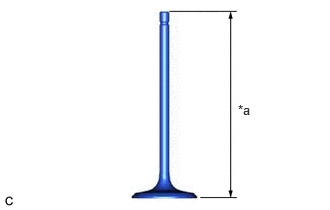
| *a | Overall Length |
Using a vernier caliper, measure the overall length of the intake valve.
- Standard Overall Length:
102.45 mm (4.03 in.)
- Minimum Overall Length:
101.95 mm (4.01 in.)
- HINT:
-
If the overall length is less than the minimum, replace the intake valve.
13715
4.INSPECT EXHAUST VALVE
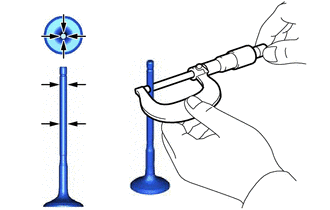
Using a micrometer, measure the diameter of the valve stem.
- Standard Valve Stem Diameter:
5.465 to 5.480 mm (0.215 to 0.216 in.)
- HINT:
-
If the valve stem diameter is not as specified, check the exhaust valve guide bush oil clearance.
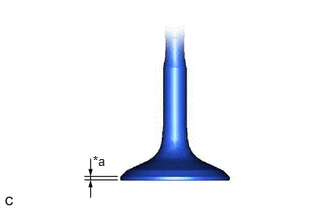
| *a | Margin Thickness |
Using a vernier caliper, measure the valve head margin thickness.
- Standard Margin Thickness:
1.0 mm (0.0394 in.)
- Minimum Margin Thickness:
0.5 mm (0.0197 in.)
- HINT:
-
If the margin thickness is less than the minimum, replace the exhaust valve.
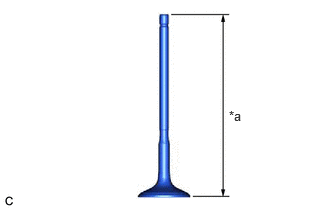
| *a | Overall Length |
Using a vernier caliper, measure the overall length of the exhaust valve.
- Standard Overall Length:
106.4 mm (4.19 in.)
- Minimum Overall Length:
105.9 mm (4.17 in.)
- HINT:
-
If the overall length is less than the minimum, replace the exhaust valve.
5.INSPECT VALVE GUIDE BUSH OIL CLEARANCE
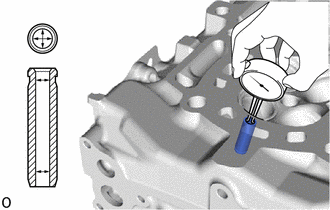
Using a caliper gauge, measure the inside diameter of the valve guide bush.
- Standard Valve Guide Bush Inside Diameter:
5.51 to 5.53 mm (0.217 to 0.218 in.)
Subtract the valve stem diameter measurement from the valve guide bush inside diameter measurement.
- Standard Oil Clearance:
Item Specified Condition Intake Side 0.025 to 0.060 mm (0.000984 to 0.00236 in.) Exhaust Side 0.030 to 0.065 mm (0.00118 to 0.00256 in.)
- Maximum Oil Clearance:
Item Specified Condition Intake Side 0.08 mm (0.00315 in.) Exhaust Side 0.10 mm (0.00394 in.)
- HINT:
- ·
Oil clearance = Valve guide bush inside - Valve stem diameter
·If the oil clearance is more than the maximum, replace the valve and valve guide bush.
6.INSPECT INTAKE VALVE SEAT
Apply a light coat of Prussian blue to the valve face.
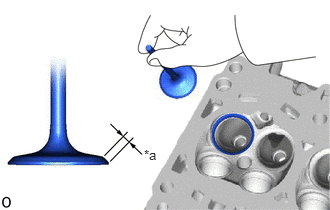
| *a | Width |
Lightly press the valve face against the intake valve seat.
- NOTICE:
-
Do not rotate the valve while pressing it.
Check the valve face and intake valve seat by using the following procedure:
If Prussian blue appears 360° around the entire intake valve face, the valve face is concentric.
- HINT:
-
If the valve face is not concentric, replace the intake valve.
If Prussian blue appears 360° around the entire intake valve seat, the intake valve seat and valve face are concentric.
- HINT:
-
If the valve face is not concentric, replace the cylinder head sub-assembly.
Measure the width of the contact area of the intake valve seat and valve face.
- Standard Width:
1.0 to 1.4 mm (0.0394 to 0.0551 in.)
7.INSPECT EXHAUST VALVE SEAT
Apply a light coat of Prussian blue to the valve face.

| *a | Width |
Lightly press the valve face against the exhaust valve seat.
- NOTICE:
-
Do not rotate the valve while pressing it.
Check the valve face and exhaust valve seat by using the following procedure:
If Prussian blue appears 360° around the entire exhaust valve face, the valve face is concentric.
- HINT:
-
If the valve face is not concentric, replace the exhaust valve.
If Prussian blue appears 360° around the entire exhaust valve seat, the exhaust valve seat and valve face are concentric.
- HINT:
-
If the valve face is not concentric, resurface the exhaust valve seat.
Measure the width of the contact area of the exhaust valve seat and valve face.
- Standard Width:
1.2 to 1.6 mm (0.0472 to 0.0630 in.)
8.INSPECT CAMSHAFT THRUST CLEARANCE
Clean the No. 1 camshaft bearing cap, No. 2 camshaft bearing cap, 2 No. 3 camshaft bearing caps, No. 4 camshaft bearing cap, camshaft housing sub-assembly and camshaft journals.
Place the intake camshaft sub-assembly and exhaust camshaft sub-assembly on the camshaft housing sub-assembly.
Install the camshaft bearing caps.
Install the camshaft housing sub-assembly.
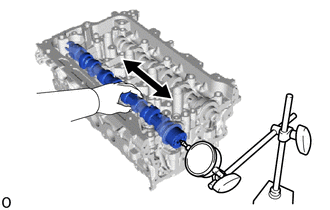
Using a dial indicator, measure the thrust clearance while moving the intake camshaft sub-assembly and exhaust camshaft sub-assembly back and forth.
- Standard Thrust Clearance:
Item Specified Condition Intake camshaft sub-assembly 0.04 to 0.17 mm (0.00157 to 0.00669 in.) Exhaust camshaft sub-assembly 0.04 to 0.17 mm (0.00157 to 0.00669 in.)
- Maximum Thrust Clearance:
Item Specified Condition Intake camshaft sub-assembly 0.22 mm (0.00866 in.) Exhaust camshaft sub-assembly 0.22 mm (0.00866 in.)
- HINT:
-
If the thrust clearance is more than the maximum, replace the camshaft housing sub-assembly. If the thrust surface is damaged, replace the camshaft.